

UK brickmaker Forterra has concluded a £140 million brick manufacturing upgrade, anchored by a £95 million overhaul of its Desford facility. The redevelopment doubles the site’s annual output to 180 million bricks while cutting carbon emissions per unit by 25%. It represents a significant structural shift in a centuries-old production method, integrating modern automation and alternative fuel trials.
Brickmaking traces its origins to sun-dried mud in 7,000 BC, with fired clay emerging around 3,500 BC in Mesopotamia. The fundamental process of moulding and firing clay remains foundational to the global construction industry. Yet, the extreme energy demands of large-scale commercial kilns compel modern manufacturers to overhaul their operations entirely.
Scaling output through its brick manufacturing upgrade
Forterra is actively addressing this tension across its 11 UK sites. Through targeted hardware upgrades, strategic product diversification, and highly localised material sourcing, the company is bridging the gap between historical manufacturing techniques and stringent net-zero emission targets.
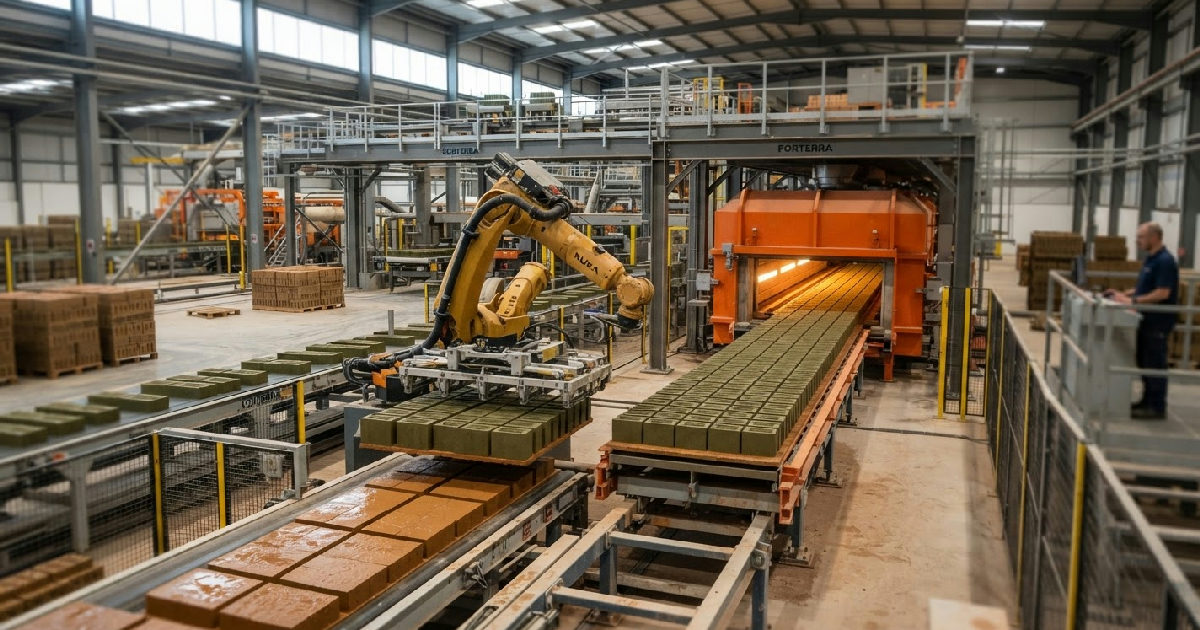
The Desford factory in Leicestershire now operates as the largest and most efficient brick plant in Europe. Commissioned in late 2022 and officially opened in May 2023, the facility added 120 million bricks to Forterra’s annual capacity. This single site upgrade increased the group’s total production volume by 22 percent.
This expanded output provides enough material to build 25,000 average family-sized homes each year. The facility’s grand opening drew support from the Brick Development Association (BDA), with CEO Keith Aldis and local MP Dr Luke Evans commending the industrial scale-up. The plant produces a varied run of red and buff bricks.
Italian engineering firm Bedeschi delivered the turnkey project, supplying an integrated system from clay preparation through to packaging. The facility incorporates robotics hardware and advanced control systems. The adoption of robotics and automated controls brings a level of precision manufacturing to a historically heavy-industrial process.
Heating efficiency sits at the core of the Desford upgrade. Engineers installed two new kilns featuring an advanced kiln-car design and enhanced thermal insulation. A new tunnel dryer replaces the standard chamber design, capturing and redistributing heat to significantly lower the plant’s overall energy requirements.
Diversifying product lines across UK facilities
Beyond the Desford expansion, Forterra directed £30 million toward upgrading its Wilnecote factory in Staffordshire. The nine-month closure and refit increased site capacity by 20 percent. This modernised facility focuses on a wider range of high-specification products, specifically boosting the output of Staffordshire blue bricks.
Market demand for alternative cladding has also driven a £12 million investment at the Accrington factory. This site now houses an automated production line capable of producing 48 million brick slips annually. The Omnia brick slip replicates the aesthetic of traditional clay while drastically reducing material waste.
Previously, creating this effect required cutting the face from an entire brick and discarding the remainder. The new Accrington line produces a unit with four slips, making the extrusion process far more material-efficient. These slips are available in a wide palette of colours, textures, and engobed finishes.
The company expanded this architectural flexibility by developing the SureBrick system. Certified by the British Board of Agrément (BBA) as A1 non-combustible, the system mounts slips directly to building facades. The lightweight format supports vertical adjustments during installation while improving overall thermal performance in commercial buildings.
Localising supply chains to secure raw materials
While Forterra modernises its extruded brick operations, its Measham site continues to run a traditional soft-mud process. This plant produces 100 million Ecostock bricks a year by throwing clay into moulds before firing. The resulting texture and detail command a premium price in the market.
The Measham factory was built to replace three older plants and has reduced its energy consumption by 50 percent through advanced heat redistribution. Furthermore, raw material wastage remains below one percent, and all water used during the manufacturing process is recycled into the system.
Operational resilience at Measham stems directly from its material sourcing strategy. Approximately 90 percent of the clay required for production originates from an on-site quarry located just 200 metres from the factory. Local sand extraction further shortens the logistical footprint required to feed the kilns.
Controlling raw material extraction at the source insulates the facility from broader supply chain volatility. By eliminating long-distance heavy haulage, the plant maintains continuous production schedules while cutting transport-related emissions. This closed-loop approach to material handling helps ensure highly predictable input costs.
Trialling hydrogen blends for heavy industry
Natural gas consumption in kilns accounts for roughly 60% of Forterra’s total carbon footprint. Addressing this base-load energy requirement remains the company’s most significant operational challenge. Grid-scale hydrogen infrastructure is likely a decade away, but industrial testing is already yielding results.
Working with industrial gas supplier Air Products, Forterra recently completed alternative fuel trials at a facility in Derbyshire. Engineers tested a blend containing 20 percent hydrogen and 80 percent natural gas. They used a standard natural gas kiln as a control environment to monitor output quality accurately.
The results confirmed that the 20 percent hydrogen mix had no adverse effect on the colour, consistency, or structural integrity of the bricks. The next phase involves converting a smaller batch kiln at Measham to run entirely on hydrogen. This smaller kiln can fire up to 12,000 bricks per cycle.
The viability of hydrogen was further demonstrated through a St Helens consortium project with Ceramics UK, where members successfully tested products in a kiln powered by 100 percent hydrogen. However, building entirely new hydrogen kilns remains prohibitively expensive. Consequently, engineers are exploring dual-fired retrofit options featuring separate burners for natural gas and hydrogen.
Cross-industry practices and material recovery
Industrial energy transitions often require hybrid solutions before achieving complete decarbonisation. While some manufacturers look toward onsite power generation, heavy ceramics production demands the intense, consistent thermal energy that only large-scale combustion or highly advanced electric kilns can supply.
Decarbonising the manufacturing process extends beyond kiln fuel. Forterra has established a partnership with LKAB Minerals to process structural waste from its Kings Dyke factory. The crushed brick is fine-milled into a reactive calcined clay, providing a low-carbon supplementary material for the cement industry.
The collaboration targets an annual output of 35,000 tonnes of calcined clay. This industrial process reduces landfill waste while supplying a critical input for lower-carbon concrete production. It highlights how material recovery can create secondary revenue streams from manufacturing byproducts.
Internally, the company extensively integrates Building Information Modelling (BIM) to track these environmental metrics. Detailed Environmental Product Declarations (EPDs) are incorporated directly into BIM software. This precise data allows construction clients to calculate the exact carbon footprint of their building designs using Forterra products.
Maintenance strategies have also evolved through the targeted recruitment of personnel from the aerospace and automotive sectors. Introducing standardised programmable logic controllers (PLCs) across all 11 UK sites helps prevent single points of failure. If a component fails at one plant, identical spares from another location can immediately restore operations.
Implications for emerging industrial markets
The evolution of Forterra’s manufacturing footprint offers clear strategic parallels for industrial developers across Africa and other emerging economies. Heavy manufacturing relies fundamentally on reliable material inputs and consistent thermal energy. The Measham plant’s hyper-localised supply chain proves that co-locating extraction and processing provides immense operational stability.
African cement and ceramics producers face similar challenges regarding energy intensity and grid reliability. While hydrogen testing remains in its infancy globally, the drive to improve kiln thermal efficiency and recover waste heat is broadly applicable. Retrofitting older kilns with modern insulation and automated control systems can deliver immediate operational savings.
Government funding delays often slow industrial decarbonisation projects in the UK, a challenge familiar to manufacturers operating in emerging markets. This underscores the necessity for companies to self-fund critical efficiency upgrades rather than waiting for structural subsidies.
Upgrading legacy manufacturing processes does not necessarily require abandoning traditional methods. By integrating digital tracking, diversifying product outputs, and securing raw materials locally, operators can scale production sustainably. Long-term industrial resilience requires continuous, pragmatic adaptation to changing energy economics and shifting market demands.
